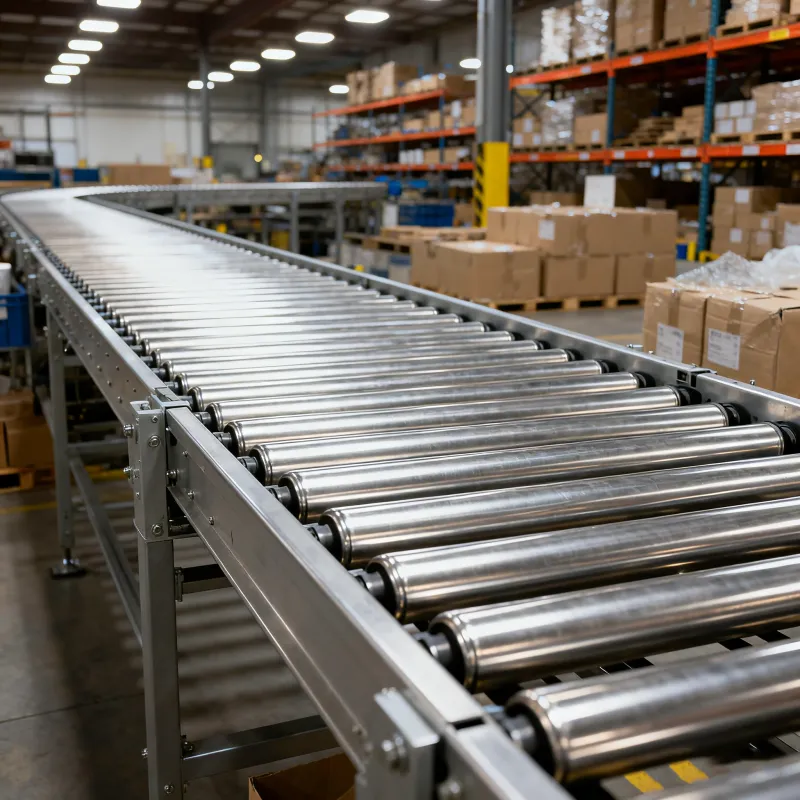
Conveying equipment solutions for demanding material handling environments
A complete conveying equipment solution is a coordinated material handling system designed around the material, conveying route, required capacity and site conditions. For mining, chemical and grain applications, the system may combine belt conveyors, bucket chain conveyors, screw conveyors, vertical lifting equipment and mesh belt conveyors.
ZhengZhou TianQi Machinery Co., Ltd. develops, manufactures and exports conveying equipment for industrial applications. The company evaluates the complete conveying route rather than treating each conveyor as an isolated machine, helping customers select suitable equipment for horizontal, inclined, vertical, high-temperature and continuous conveying requirements.
The configuration of a conveying system depends on the distance between process points, the characteristics of the conveyed material, the required throughput, the conveying direction and the available installation space. Based on these factors, different equipment types can be used individually or combined into an integrated system.
| Equipment type | Typical conveying role | Application relevance |
|---|---|---|
| Belt conveyor | Continuous movement of bulk materials over horizontal or inclined routes | Suitable for material transfer in mining, chemical and grain handling processes |
| Bucket chain conveyor | Vertical or elevation-changing movement of bulk materials | Helps connect different process levels where vertical lifting is required |
| Screw conveyor | Controlled conveying of bulk materials through a compact route | Can be incorporated where space-efficient material transfer is needed |
| Vertical lifting equipment | Transfer of materials between different elevations | Supports multi-level production and storage layouts |
| Mesh belt conveyor | Horizontal, inclined or vertical conveying with a metal mesh belt | Suitable for high-temperature, chemical cooling and food processing conveying lines |

The metal mesh belt conveyor is one of the key equipment options in a complete conveying equipment solution. ZhengZhou TianQi Machinery produces this conveyor using carbon steel, 201 stainless steel or 304 stainless steel, depending on the application requirements.
Its configuration supports horizontal, inclined and vertical conveying in layouts where route flexibility, temperature resistance and continuous material movement are important. The conveyor can handle materials with temperatures up to 600°C and provides a stated conveying capacity of up to 526 m³/h.
Conveying equipment can be arranged to transfer bulk materials across horizontal, inclined and vertical sections of a mining process.
Stainless steel mesh belt configurations can be considered for chemical conveying and cooling processes where material and temperature conditions require suitable equipment selection.
Belt, screw, bucket chain and vertical conveying equipment can be coordinated to support continuous bulk material movement in grain-related layouts.
Durable metal mesh belt conveyors can be used for food processing production lines where continuous conveying and appropriate material selection are required.
Founded in 2013 and headquartered in Henan, China, ZhengZhou TianQi Machinery Co., Ltd. focuses on the research, production and export of conveying equipment. Its product range includes belt conveyors, bucket chain conveyors, screw conveyors, vertical lifting equipment and mesh belt conveyors.
Precise conveying. Driving the future.
ZhengZhou TianQi Machinery applies a technology-led, quality-focused approach to conveying equipment design, helping customers evaluate complete solutions for mining, chemical, grain and related material handling applications.


 426
|
 ZhengZhou TianQi Machinery industrial conveyor equipment market conveyor equipment trends intelligent conveying system equipment reliability international procurement
452
|
ZhengZhou TianQi Machinery conveyor equipment purchasing mistakes lifecycle cost of conveyor systems conveyor system stability supplier evaluation
240
|
ZhengZhou TianQi Machinery mining conveyor equipment chemical conveyor equipment grain conveyor equipment conveyor system configuration
257
|
ZhengZhou TianQi Machinery conveyor equipment selection conveying capacity material characteristics industrial conveyor
170
|
ZhengZhou TianQi Machinery Co., Ltd. conveying equipment selection conveying capacity material characteristics equipment procurement parameters