Conveyor Equipment Solutions
ZhengZhou TianQi Machinery Co., Ltd. provides conveyor equipment solutions for mining, chemical and grain handling applications. The product range includes belt conveyors, bucket conveyors, screw conveyors, vertical elevators and roller conveyor systems, helping businesses organize material movement according to distance, material characteristics, lifting height, throughput and line integration requirements.

The appropriate conveyor equipment solution depends on the operating conditions and layout of the material-handling line. Key considerations include the conveying distance, material properties, required lifting height, expected throughput, product dimensions and the way the equipment must connect with existing or dedicated machinery. A suitable combination may use one conveyor type or integrate several systems to support continuous and stable transfer.
| Equipment type | Typical role | Relevant application focus |
|---|---|---|
| Belt conveyor | Continuous transport over suitable horizontal or inclined routes | Mining, chemical and grain material handling |
| Bucket conveyor | Vertical or elevated transfer of bulk materials | Applications requiring controlled lifting |
| Screw conveyor | Enclosed or controlled movement of suitable bulk materials | Chemical and grain processing lines |
| Vertical elevator | Material elevation between different production or storage levels | Facilities where vertical space and lifting height are important |
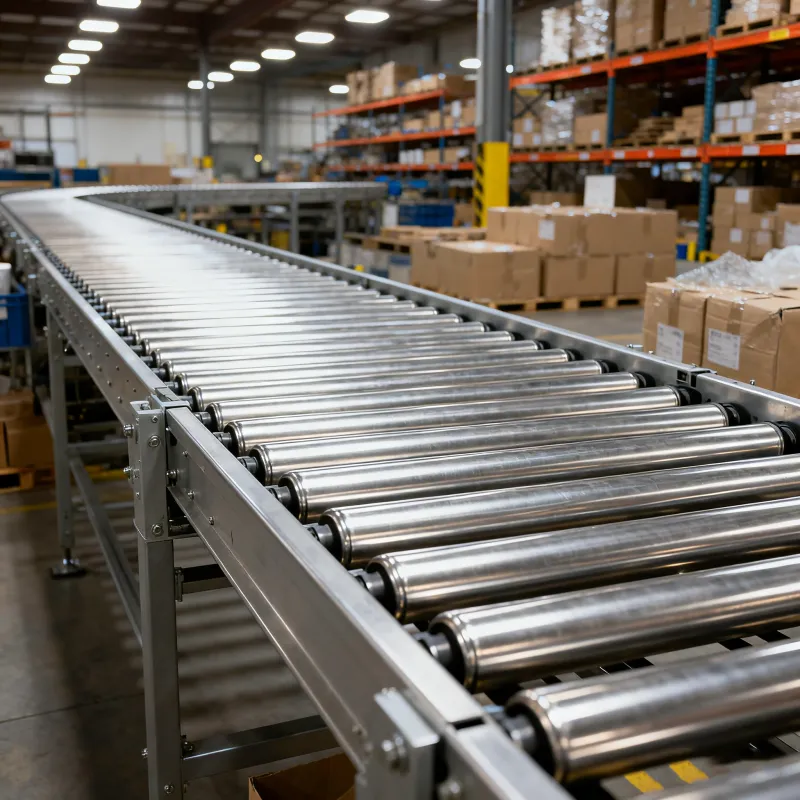
| Roller conveyor system | Smooth transport of flat-bottomed items such as boxes, pallets and totes | Unit-load handling and integrated production or logistics lines |
The roller conveyor system from ZhengZhou TianQi Machinery is designed for efficient handling of flat-bottomed products, including boxes, pallets and totes. Its main structure can include drive rollers, a conveyor frame, support legs and a power unit, providing stable movement for applications that require smooth transfer and high handling efficiency.
Depending on the line layout and operating requirements, the system is available in powered and non-powered configurations. It can support horizontal, inclined and curved conveying, while its modular structure allows connection with other conveyors or specialized equipment.
Conveying width can be customized from 150 mm to 1,200 mm, with multiple roller diameter options available to match specific handling requirements.
A robust structure, suitable drive arrangement and carefully selected configuration support smooth conveying, high throughput and reliable day-to-day operation.
The modular design makes it easier to integrate the roller conveyor system with other conveyors and dedicated equipment in an automated handling line.
For mining, chemical and grain material handling, conveyor selection should reflect the material form, required conveying path and line capacity. Roller conveyor systems are particularly suitable for flat-bottomed unit loads, while bulk-material applications may require belt, bucket, screw or vertical conveying equipment. When several transfer functions are needed, these systems can be evaluated as an integrated conveyor equipment solution.
The final configuration should be determined according to the material, product dimensions, conveying direction, throughput and connection requirements of the specific line.
Founded in 2013 and headquartered in Henan, China, ZhengZhou TianQi Machinery Co., Ltd. focuses on the research, manufacture and export of conveyor equipment. The company provides belt conveyor, bucket conveyor, screw conveyor, vertical elevator and roller conveyor systems for customers in mining, chemical, grain and related material-handling sectors.
With a professional research and development team, quality control procedures, technical support and responsive after-sales service, TianQi Machinery supports customers in evaluating practical conveyor configurations. The company reports a 98% on-time delivery rate and serves international markets including Europe, North America, Southeast Asia and the Middle East.
“Precise conveying, driving the future” reflects TianQi Machinery’s focus on technology-led development and quality-based conveyor equipment solutions.
 245
|
 ZhengZhou TianQi Machinery Co., Ltd. conveyor equipment purchasing equipment price and specifications supplier evaluation conveyor system risks
80
|
TianQi Machinery conveyor system design equipment configuration process requirement analysis technical solution
145
|
ZhengZhou TianQi Machinery Co., Ltd. conveyor equipment solutions mesh belt conveyor material handling equipment conveyor equipment export
160
|
TianQi Machinery foreign trade digital marketing tool integration data collaboration marketing conversion
407
|
ZhengZhou TianQi Machinery industrial conveyor equipment selection material characteristics conveying capacity conveying distance