Conveyor Equipment Solutions
Conveyor equipment selection should reflect the material characteristics, conveying direction, required capacity, lifting height and operating environment. ZhengZhou TianQi Machinery provides conveying equipment solutions covering belt conveyors, bucket conveyors, screw conveyors, vertical lifting conveyors and mesh belt conveyors for industrial material handling applications.

Conveyor equipment solutions are integrated decisions about conveying equipment, layout and configuration based on the way materials need to move through a production or handling process. A suitable system considers whether materials must be conveyed horizontally, at an incline or vertically, as well as the operating conditions that may affect equipment construction and maintenance.
For applications involving high temperature, chemical processing, food production or complex plant layouts, the conveyor structure and material selection are especially important. ZhengZhou TianQi Machinery develops and supplies conveying equipment for mining, chemical, grain and other industrial sectors, with options that can be adapted to different conveying requirements.
| Conveyor type | Typical selection considerations | Application context |
|---|---|---|
| Belt conveyor | Continuous movement over horizontal or inclined routes | General bulk-material conveying |
| Bucket conveyor | Vertical or high-angle lifting of suitable bulk materials | Material elevation and transfer |
| Screw conveyor | Controlled movement through a compact, enclosed conveying route | Process and bulk-material handling |
| Vertical lifting conveyor | Movement between different production or storage levels | Space-conscious vertical transfer |
| Mesh belt conveyor | High-temperature, cooling, drying or continuous process conveying requirements | Chemical, food and industrial production lines |
The final equipment configuration should be determined according to the material, conveying route, process conditions and system requirements.
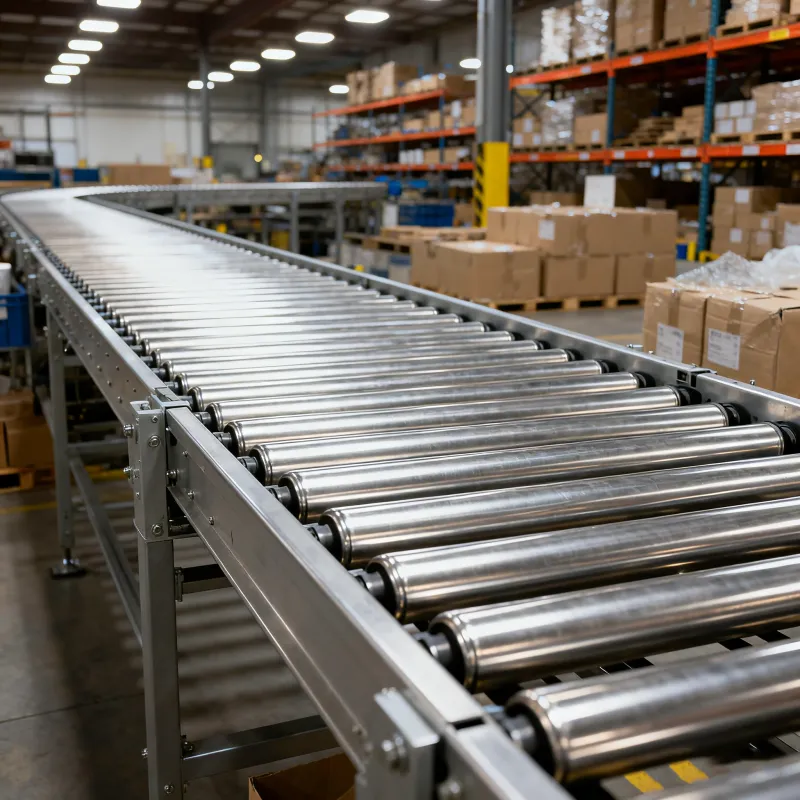
The metal mesh belt conveyor from ZhengZhou TianQi Machinery is designed for continuous material conveying in horizontal, inclined and vertical layouts. It can be manufactured from carbon steel, 201 stainless steel or 304 stainless steel, allowing the equipment configuration to be considered according to the application environment.
The conveyor is suitable for conveying materials with temperatures up to 600°C. Its stated conveying capacity can reach 526 m³/h, while the conveying inclination can reach 60 degrees. These parameters provide a reference for evaluating the equipment in high-temperature industrial drying, chemical cooling and food-processing conveying scenarios.
The traction chain and load-bearing chain are separated, helping simplify the structure and make routine maintenance more convenient.
Rolling bearings on the rollers are designed to reduce friction by a stated 55%–65%, supporting lower energy consumption during operation.
Wear-resistant alloy steel components are used to support long service life in demanding conveying conditions.
Horizontal, inclined and vertical conveying configurations can be considered for installations with complex spatial layouts.
ZhengZhou TianQi Machinery Co., Ltd. focuses on the research, production and export of conveying equipment. Its solution scope includes belt conveyors, bucket conveyors, screw conveyors, vertical lifting conveyors and mesh belt conveyors for material handling applications across mining, chemical, grain and related industries.
For the metal mesh belt conveyor, TianQi Machinery provides support from non-standard design to system integration. The company also states a 98% on-time delivery rate and a 2-hour response commitment for customer service.
By combining application requirements with equipment structure and operating conditions, customers can evaluate a conveying system that is better aligned with their material-handling process.

 105
|
 ZhengZhou TianQi Machinery conveyor equipment procurement project requirements checklist custom conveyor solution equipment technical parameters
134
|
ZhengZhou TianQi Machinery Co., Ltd. foreign trade marketing trends data-driven customer management customer lifecycle management growth model
237
|
ZhengZhou TianQi Machinery Co., Ltd. foreign trade intelligent marketing SaaS platform customer conversion digital management
158
|
ZhengZhou TianQi Machinery conveying equipment selection material characteristics conveying distance and capacity industrial equipment procurement
426
|
ZhengZhou TianQi Machinery industrial conveyor equipment market conveyor equipment trends intelligent conveying system equipment reliability international procurement