Industrial Conveying Equipment Solutions
The appropriate conveying equipment depends on the material being handled, conveying distance, lifting height, required capacity and operating conditions. ZhengZhou TianQi Machinery Co., Ltd. provides conveying equipment solutions for mining, chemical processing and grain handling, with product options including roller conveyor systems, belt conveyors, bucket elevators, screw conveyors and vertical lifts.

Industrial conveying equipment should be selected according to the complete handling process rather than a single equipment name. A clear evaluation of the following factors helps align the system configuration with the application:
Consider whether the material consists of flat-bottomed items, bulk materials or other product forms, as well as the handling conditions required by the process.
The required distance, direction and layout influence whether the system should be horizontal, inclined, curved or integrated with lifting equipment.
Throughput requirements and the expected flow of products or materials should be reviewed before defining the conveyor configuration.
The working environment, equipment integration requirements and maintenance expectations should be included in the selection process.
Different conveying systems address different material handling conditions. The following overview can support an initial comparison before detailed engineering and configuration.
| Equipment type | Selection focus | Relevant application context |
|---|---|---|
| Roller conveyor systems | Flat-bottomed items, layout, width, roller diameter and powered or non-powered operation | Boxes, pallets and totes in integrated handling lines |
| Belt conveyors | Material form, conveying route, distance and required capacity | Material handling processes in mining, chemical and grain applications |
| Bucket elevators | Lifting height, material characteristics and vertical transfer requirements | Processes that require vertical movement of materials |
| Screw conveyors | Material condition, conveying distance and process arrangement | Material transfer within industrial processing lines |
| Vertical lifts | Lifting height, load requirements and connection with other equipment | Vertical transfer and multi-level conveying arrangements |
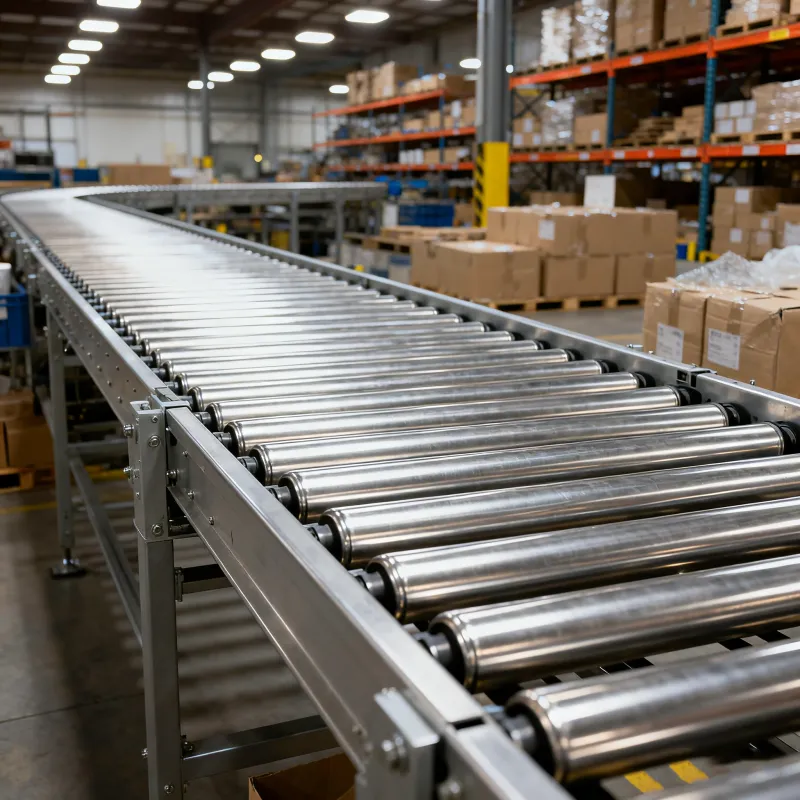
A roller conveyor system is designed for the efficient movement of flat-bottomed items such as boxes, pallets and totes. Its main structure includes rollers, a frame, support legs and a power unit. The system can support high-throughput handling, fast transfer and smooth operation when properly matched to the product and line layout.
ZhengZhou TianQi Machinery Co., Ltd. offers both powered and non-powered configurations. Roller conveyor systems can be arranged for horizontal, inclined or curved conveying, allowing them to connect with other conveyors or dedicated equipment in a modular production or handling line.
When selecting equipment for mining material handling, review the material characteristics, conveying distance, required capacity and operating conditions. Belt conveyors and other suitable systems can then be evaluated against the complete process route.
Chemical logistics and processing lines require equipment selection based on the material and operating environment. The final configuration should reflect the conveying route, capacity and integration requirements.
For grain handling applications, the conveying method should be considered together with material flow, transfer distance, elevation changes and the overall production line arrangement.
Selection principle: start with the material, route and operating requirements, then determine the appropriate conveyor type, configuration and integration method. This approach helps create a conveying equipment solution that is clearer to evaluate and easier to adapt to the actual application.
Founded in 2013 and headquartered in Henan, China, ZhengZhou TianQi Machinery Co., Ltd. focuses on the research, production and export of conveying equipment. Its product range covers roller conveyor systems, belt conveyors, bucket elevators, screw conveyors and vertical lifts for industrial material handling applications.
With a professional research and development team, quality control procedures and technical support, TianQi Machinery serves customers in mining, chemical and grain-related industries. The company reports a 98% on-time delivery rate and responsive after-sales service, providing a practical foundation for evaluating and implementing conveying equipment solutions.

 422
|
 ZhengZhou TianQi Machinery Co., Ltd. conveyor equipment procurement equipment quotation system matching maintenance cost
285
|
ZhengZhou TianQi Machinery Co., Ltd. conveyor equipment supplier conveyor solutions roller conveyor system conveyor equipment export
144
|
ZhengZhou TianQi Machinery Co., Ltd. customs data email marketing CRM workflow foreign trade lead generation
105
|
ZhengZhou TianQi Machinery conveyor equipment procurement project requirements checklist custom conveyor solution equipment technical parameters
386
|
ZhengZhou TianQi Machinery conveyor equipment conveying solutions industrial material handling conveyor equipment export