Industrial Material Handling
Industrial conveyor equipment solutions are systems designed to move bulk materials safely, consistently and efficiently within mining, chemical, grain and construction operations. The appropriate solution depends on the material characteristics, required conveying distance, lifting height, throughput and operating environment.
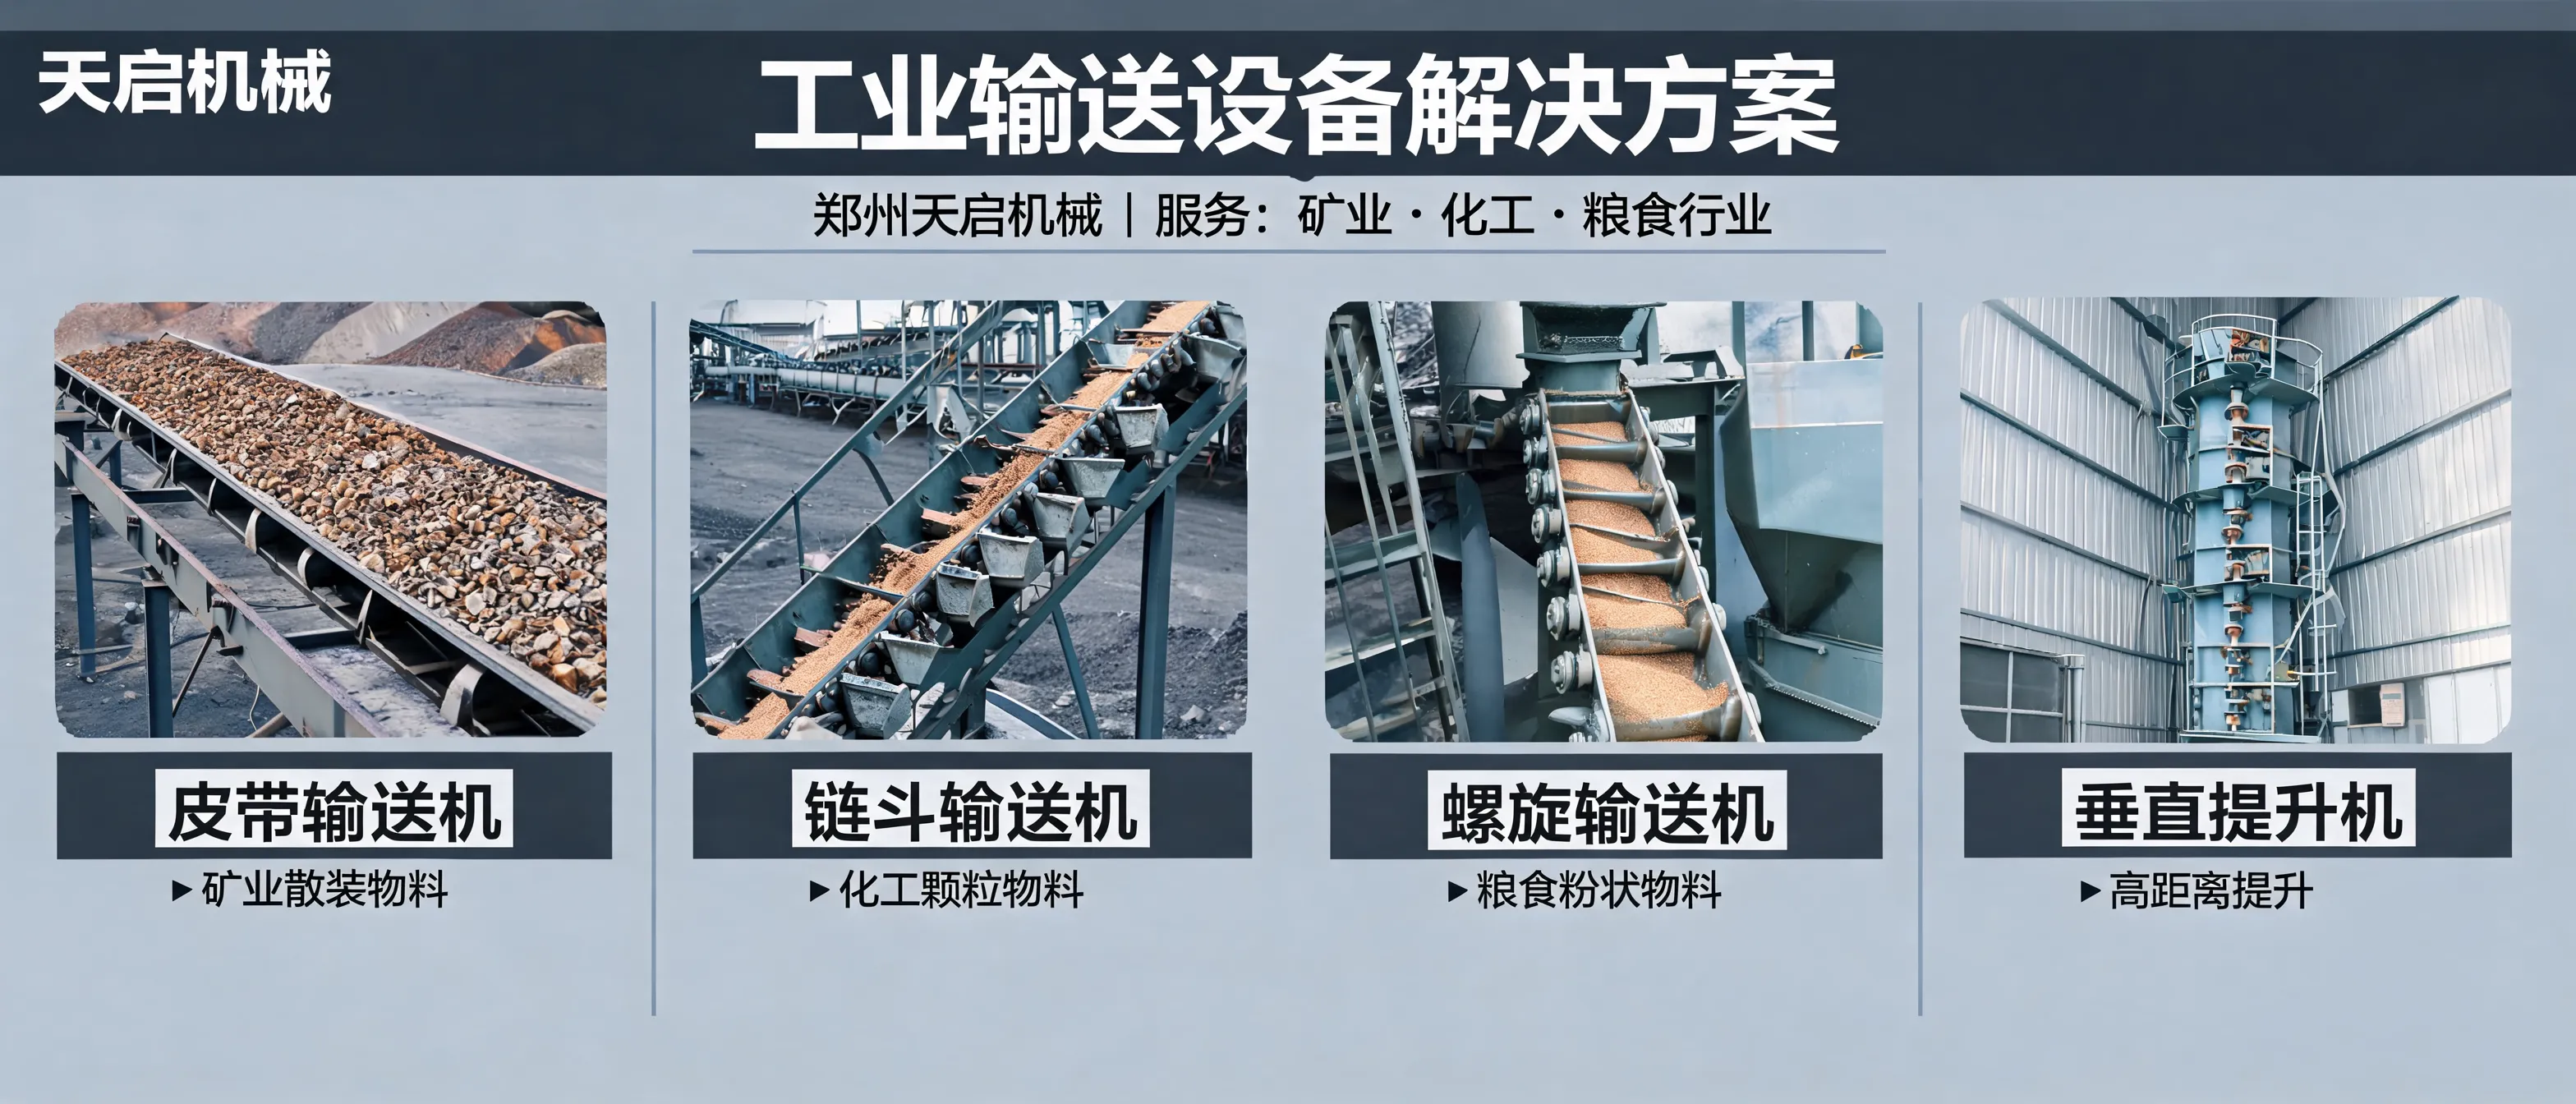
ZhengZhou TianQi Machinery Co., Ltd. develops, manufactures and exports conveying equipment for industrial applications. Its portfolio includes belt conveyors, bucket conveyors, screw conveyors and vertical elevators, with configurable equipment options for different process requirements.
Conveyor selection should begin with the operating conditions rather than with a single equipment type. A practical assessment normally considers the following factors:
Different conveyor technologies address different material handling tasks. ZhengZhou TianQi Machinery provides equipment categories that support continuous conveying, lifting and process integration across a range of industrial applications.
| Equipment type | Typical selection focus | Relevant applications |
|---|---|---|
| Belt conveyors | Continuous transport, conveying distance, capacity and belt configuration | Mining, chemical, grain and construction material handling |
| Bucket conveyors | Vertical or elevated movement of bulk materials | Processes requiring controlled lifting and transfer |
| Screw conveyors | Controlled movement within a compact conveying route | Bulk material handling and process conveying |
| Vertical elevators | Lifting height and vertical transfer requirements | Facilities where available floor space or elevation changes affect layout |
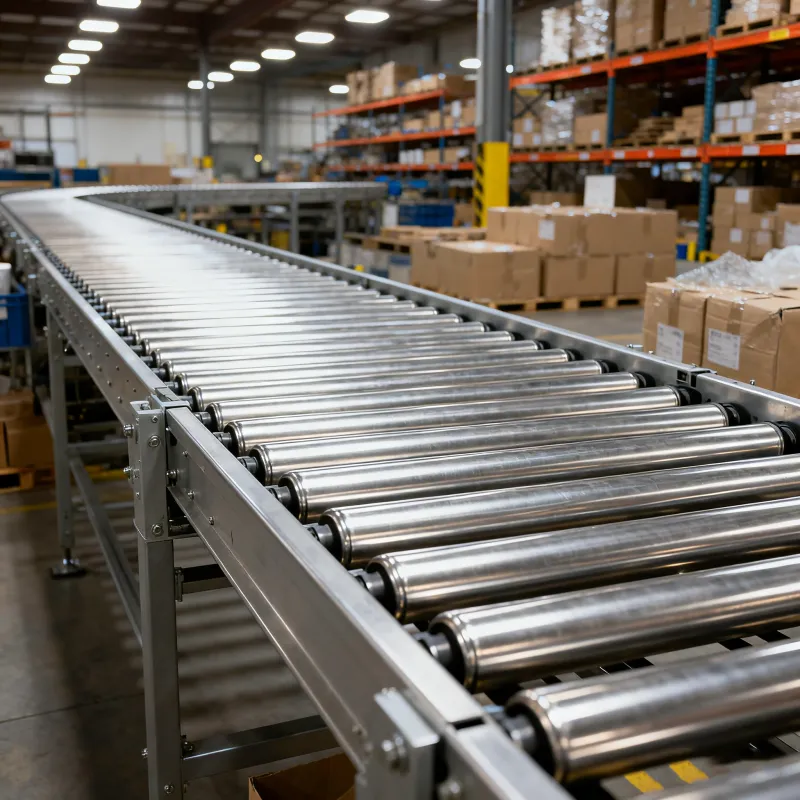
The HQ-200 heavy-duty belt conveyor is designed for high-intensity material conveying in mining, chemical, grain and construction applications. Its configurable structure supports trough, flat, inclined and curved belt arrangements, allowing the system to be adapted to different process layouts.
The system is developed for stable, low-noise and energy-efficient operation, supporting reliable material transfer while helping manage operating requirements.
For industrial conveyor equipment, dependable performance is supported by manufacturing control, installation guidance and ongoing service. ZhengZhou TianQi Machinery applies quality controls from raw material inspection through final testing. Its manufacturing system is certified to ISO 9001, ISO 14001 and ISO 45001 standards.
Whether the requirement involves mining materials, chemical products, grain or construction materials, an industrial conveyor solution should match the material, route and operating environment. With more than ten years of experience in conveying equipment development, manufacturing and export, ZhengZhou TianQi Machinery Co., Ltd. provides configurable equipment and service support for customers seeking reliable material handling solutions.

 200
|
 ZhengZhou TianQi Machinery
industrial conveyor equipment
conveyor selection
belt conveyor
screw conveyor
176
|
ZhengZhou TianQi Machinery Co., Ltd.
conveyor equipment projects
conveyor solution design
equipment delivery
after-sales service
442
|
ZhengZhou TianQi Machinery Co., Ltd.
belt conveyor
chain bucket conveyor
screw conveyor
vertical elevator
292
|
ZhengZhou TianQi Machinery Co., Ltd.
SaaS marketing platform selection
foreign trade enterprises
feature fit
implementation capability
133
|
ZhengZhou TianQi Machinery Co., Ltd.
foreign trade marketing trends
data-driven customer management
customer lifecycle management
growth model