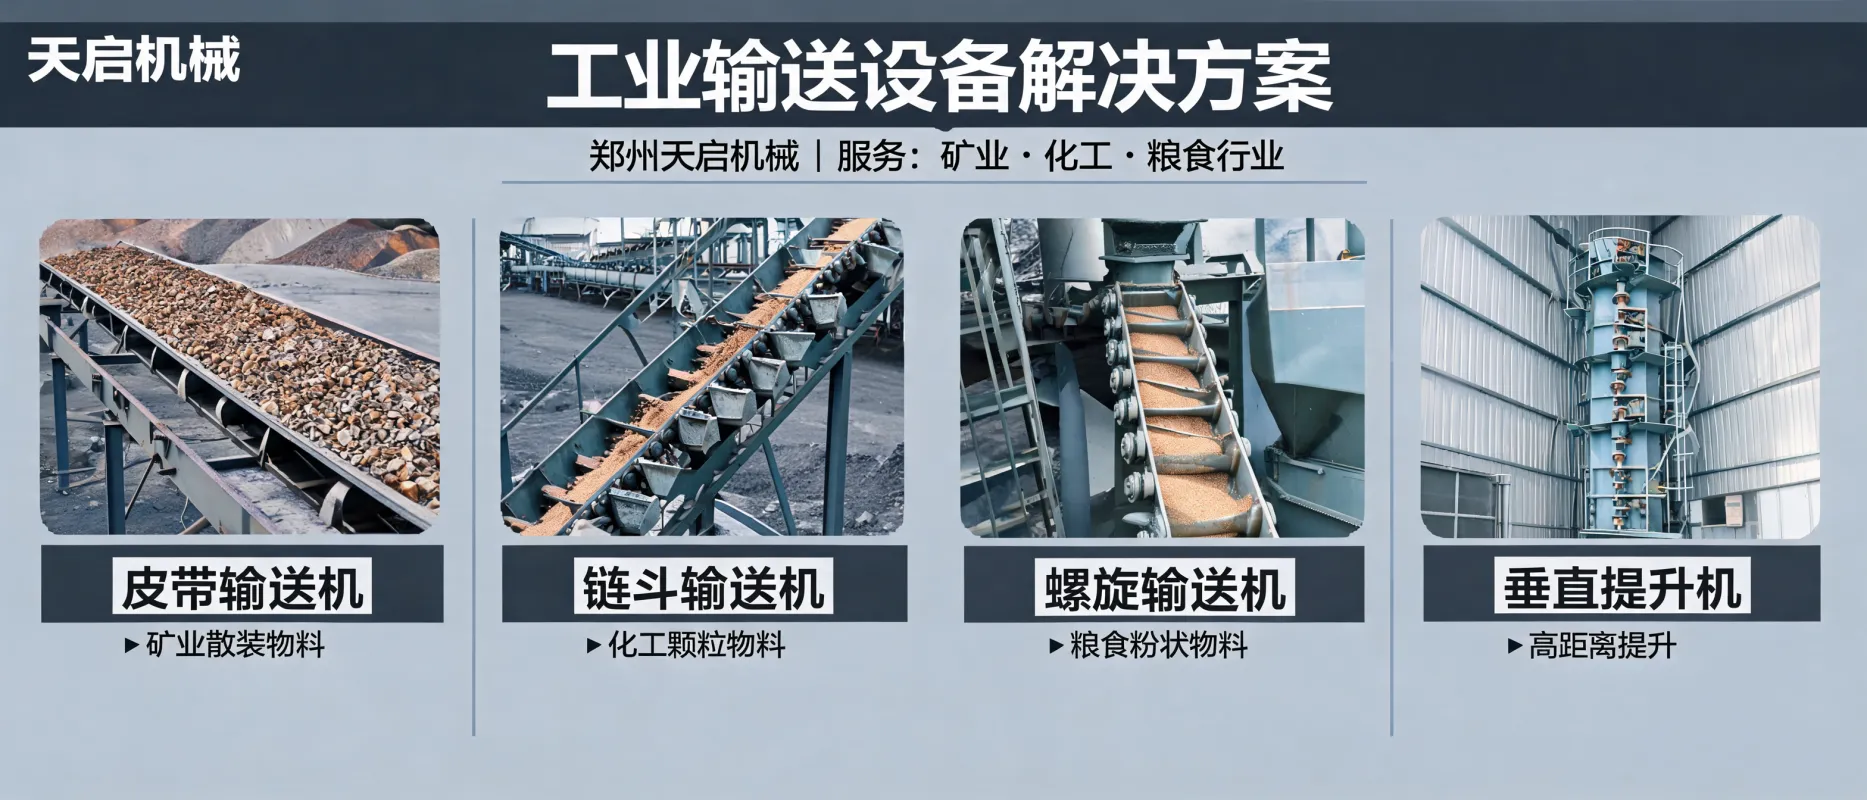
Integrated conveying equipment solutions for demanding material-handling processes
An integrated conveying equipment solution is a coordinated material-handling system designed around the characteristics of the conveyed material, required capacity, conveying distance and process layout. Instead of selecting a single machine in isolation, the complete solution considers how equipment works together from feeding and transfer to elevation and discharge.
ZhengZhou TianQi Machinery Co., Ltd. provides conveying equipment solutions for mining, chemical, grain and other industrial applications. Its equipment portfolio includes belt conveyors, chain bucket conveyors, screw conveyors and vertical conveyors, supporting different conveying routes and process requirements.
The equipment configuration should match the material and the operating environment. Key considerations include:

A conveying solution can combine different equipment types according to the material-handling route. The appropriate selection depends on the application rather than on a one-size-fits-all configuration.
| Equipment type | Role within a conveying solution |
|---|---|
| Belt conveyor | Continuous conveying for material transfer over configured horizontal, inclined, curved or flat routes. |
| Chain bucket conveyor | Part of the equipment range available for conveying applications that require a chain-and-bucket configuration. |
| Screw conveyor | Part of the equipment range for process layouts requiring screw-based material transfer. |
| Vertical conveyor | Part of the equipment range for material elevation within an integrated conveying route. |
The HQ-200 heavy-duty belt conveyor is designed for high-intensity material conveying in mining, chemical, grain and construction applications. It can be configured to suit different process layouts and conveying conditions.
TianQi Machinery’s conveying equipment solutions are intended for material-handling scenarios in:
ZhengZhou TianQi Machinery applies quality control from raw-material inspection through final testing. Its manufacturing and management systems are certified to ISO 9001, ISO 14001 and ISO 45001, supporting consistent quality, environmental management and occupational health and safety practices.
The HQ-200 heavy-duty belt conveyor includes a 12-month warranty, professional installation guidance and lifetime maintenance support. TianQi Machinery also provides a stated two-hour customer-service response and global technical support for customers evaluating or operating its conveying equipment.
A practical integrated solution starts with the process. By matching conveyor type, capacity, distance, material and layout, ZhengZhou TianQi Machinery helps industrial users define a conveying system that is aligned with their handling requirements.

 160
|
 TianQi Machinery foreign trade digital marketing tool integration data collaboration marketing conversion
379
|
ZhengZhou TianQi Machinery Co., Ltd. customs data application marketing emails qualified inquiries foreign trade case
245
|
ZhengZhou TianQi Machinery Co., Ltd. conveyor equipment purchasing equipment price and specifications supplier evaluation conveyor system risks
134
|
ZhengZhou TianQi Machinery Co., Ltd. foreign trade marketing trends data-driven customer management customer lifecycle management growth model
98
|
ZhengZhou TianQi Machinery Co., Ltd. foreign trade customer acquisition lead management customer follow-up foreign trade marketing pain points